Written by Marcus Vance – Lead Acoustic & Filtration R&D Engineer at Havenseek Industrial Vacuum Cleaner, 16 years of hands-on experience in industrial dust fluid dynamics, having audited 450+ concrete grinding and stone fabrication plants across 42 countries.
Did you know that 68% of contractors using a supposedly certified H13 HEPA vacuum cleaner still fail surprise air quality inspections? According to 2025–2026 occupational safety audit reports, fine concrete dust easily escapes through cheap plastic housing seams. Buying a fake machine puts your workers in danger and exposes your business to brutal six-figure government fines. This engineering guide reveals how to stop deadly bypass leaks and select a truly reliable unit.
In my 16 years testing dust extractors at Havenseek Industrial Vacuum Cleaner, I have seen buyers waste thousands on hollow marketing claims. Navigating strict OSHA silica dust rules requires real mechanical durability, not just a paper sticker on a filter box. When you invest in an industrial compliant dust extractor, you need guaranteed negative pressure and zero air leakage under heavy grinding loads.
Why is this article worth reading to the very end? You will get my exact $800 engineering audit blueprint used by top North American and European contractors. I will show you how to verify real filtration certificates, calculate exact airflow for your grinders, and double your filter lifespan using an H13 HEPA vacuum cleaner built to meet rigorous workplace air quality standards. Every single section gives you actionable formulas and teardown secrets using an H13 HEPA vacuum cleaner that saves money.
Verified capture rate at 0.3 microns MPPS under full aerosol photometer load testing.
Federal fine for willful or repeated silica exposure violations on commercial jobsites.
Required suction volume per inch of grinding wheel diameter for OSHA Table 1 compliance.
Quick Executive Summary: Key Engineering Takeaways
- Zero Bypass Architecture: A certified filter is useless if the steel drum flange leaks. Always demand closed-cell EPDM sponge gaskets and heavy-duty steel pressure clamps.
- Three-Stage Cyclonic Separation: Pre-separating 92% of heavy concrete dust before it hits your PTFE pre-filter prevents sudden suction drops during continuous floor grinding.
- Loaded Airflow vs. Free Air: Never buy based on open-inlet CFM alone. High static water lift (above 90 inches H2O) keeps dust moving through 30-foot anti-static hoses.
- Closed-Bag Disposal: Using a continuous Longopac bagging system eliminates secondary dust clouds when operators empty toxic crystalline silica on site.
- 1. The 2026 Regulatory Reality & OSHA Rules
- 2. H13 HEPA Vacuum vs. Standard Shop Vac
- 3. Inside the Lab: Why H13 Filters Fail Testing
- 4. Core Engineering Evaluation Benchmarks
- 5. Fluid Dynamics & Anti-Clogging Design
- 6. Single-Phase Turbines vs. 3-Phase Blowers
- 7. Safe Disposal & Continuous Bagging Systems
- 8. Exact CFM Math for Concrete Grinders
- 9. Tool-to-Vacuum Matching Matrix
- 10. Jobsite Setup, Grounding & Shrouds
- 11. Real-World B2B Case Studies & ROI
- 12. 5 Costly Sourcing Mistakes to Avoid
- 13. Frequently Asked Questions (B2B FAQ)
- 14. Conclusion & Factory Engineering Support
1. The 2026 Regulatory Reality: Why OSHA Silica Dust Rules Are Crushing Under-Spec’d Contractors
1.1 Decoding 29 CFR 1926.1153: The Brutal Math of 50 μg/m³ PEL and 25 μg/m³ Action Levels
Most site managers underestimate how tiny a lethal dose of silica really is. Achieving 29 CFR 1926.1153 Table 1 compliance means keeping airborne dust below the strict respirable crystalline silica PEL 50 ug/m3 over an eight-hour shift. If your workshop hits the crystalline silica action level 25 ug/m3, mandatory medical surveillance and air testing kick in immediately.
To visualize this volume, imagine throwing a single packet of artificial sweetener into an Olympic-sized swimming pool. That microscopic concentration equals fifty micrograms per cubic meter of air. Without an industrial-grade H13 HEPA vacuum cleaner capturing dust right at the blade, dry grinding concrete exceeds this limit in less than ninety seconds.
1.2 The 2025–2026 Enforcement Surge: Financial Penalties and Contract Disqualifications
Federal inspectors no longer give polite warnings for dusty workshops. Under updated federal enforcement guidelines, a single serious citation costs $16,550, while the maximum OSHA willful violation penalty 2026 reaches a staggering $165,514 per infraction. In 2025 alone, construction and stone fabrication inspections rose by 22% across North America.
1.3 Why Meeting Workplace Air Quality Standards Is Your Strongest B2B Bidding Advantage
Smart B2B buyers treat strict workplace air quality standards as a profit driver rather than an annoying expense. General contractors for hospitals, semiconductor plants, and government infrastructure now demand serialized filter test certificates before letting subcontractors onto the jobsite. Running a documented, leak-free dust fleet wins you high-margin contracts that cheap competitors cannot legally bid on.
2. What Is the Difference Between an H13 HEPA Vacuum Cleaner and a Standard Shop Vac?
Buyers ask me every week: What is the difference between an H13 HEPA vacuum cleaner and a standard shop vac? A hardware-store wet/dry vac is built to pick up wood chips and screws, not invisible lung-scarring minerals. Standard commercial vacuums blow sub-micron quartz particles straight through their exhaust ports, turning your machine into a toxic dust cannon.
2.1 EN 1822 vs. Marketing Hype: Understanding 99.95% Efficiency at 0.3 Microns MPPS
Retail boxes love printing “HEPA-like” on cheap paper cartridges. True medical-grade compliance requires verified EN 1822 H13 filtration efficiency 99.95% tested at the Most Penetrating Particle Size. This guarantees reliable 0.3 micron MPPS particle retention, stopping the exact aerodynamic particle size that bypasses human nasal hairs and embeds deep inside lung alveoli.
2.2 M-Class vs. H-Class and North American HEPA Equivalency
When comparing an European M-Class vs H-Class dust extractor rating, M-Class captures 99.9% of dust for general masonry, whereas H-Class (equipped with H13 or H14 media) captures 99.995% for carcinogenic silica and lead. Under strict North American OSHA silica dust rules, pairing a cyclonic pre-separator with an individually tested H13 cartridge bridges both global standards seamlessly.
3. Inside the Lab: Why Do Some H13 HEPA Filters Fail Workplace Air Quality Standards During Testing?
3.1 The Dirty Secret of “Filter Bypass”: When a Certified Cartridge Sits in a Leaky Housing
During factory teardowns, clients often ask: Why do some H13 HEPA filters fail workplace air quality standards during testing? In 90% of failed audits I have investigated, the fiberglass filter media itself was not punctured. Instead, the culprit was severe false HEPA filter bypass leakage around the mounting flange.
Air always takes the path of least resistance. When a budget vacuum pulls 95 inches of water lift, thin plastic motor heads warp by 0.8 millimeters. Unfiltered silica dust sucks straight through that microscopic gap, bypassing the filter completely while leaving the cartridge looking brand new.
3.2 How We Conduct DOP/PAO Aerosol Photometer Testing on Every Unit
At Havenseek Industrial Vacuum Cleaner, we never rely on raw media supplier paperwork alone. Every assembled H13 HEPA vacuum cleaner undergoes rigorous DOP PAO aerosol leak testing inside our acoustic test chamber. We inject atomized Polyalphaolefin oil droplets into the intake and scan the exhaust stream with a laser photometer to verify less than 0.05% total penetration.
3.3 Sealing the Weakest Link: EPDM Sponge Rubber Gaskets and Heavy-Gauge Steel Clamps
To eliminate frame warping forever, we machine flat steel seating rings and bond a 12mm closed-cell EPDM sponge rubber housing gasket directly onto the filter rim. Drop-forged stainless steel toggle latches pull the motor head down with 400 Newtons of even compression. Even after five years of rough truck transport, the seal remains 100% airtight.
4. Our Core Engineering Evaluation Criteria: 4 Benchmarks Every B2B Buyer Must Demand
When evaluating an industrial dry dust extractor wholesale supplier, looking at glossy catalog photos will get you burned. Whether you run a rental fleet or distribute equipment regionally, use these four factory engineering benchmarks to separate real industrial builds from dressed-up commercial toys.
4.1 Individual Serialized H13 Test Certificates vs. Generic Batch Papers
Never accept a photocopy of a three-year-old filter test report. A genuine compliant dust extractor ships with a serialized metallic plate on each H13 cartridge displaying its exact pressure drop and aerosol penetration percentage. If a supplier cannot match the filter serial number to a laser test log, walk away immediately.
4.2 Pleat Spacing Geometry and Fiberglass Media Depth
Dishonest factories cram 300 pleats into a tiny cylinder so they can advertise massive square footage. However, tight filter surface area media pleat spacing traps fine concrete dust between the folds, creating a solid cement brick within twenty minutes. We engineer a 4.2mm open pleat pitch that lets heavy silica cakes drop cleanly during pulse purging.
4.2.1 Hot-Melt Glue Bead Stabilization in High-Static Environments
Under high negative pressure, deep filter pleats tend tobunch together and tear along the crease. By applying spiral polyamide hot-melt glue beads across both the inner wire mesh and outer hydrophobic surface, we lock every single pleat in place. This structural bracing prevents media collapse during violent reverse-air shockwaves.
5. Fluid Dynamics & Anti-Clogging Design: Engineering a Non-Stop Compliant Dust Extractor
5.1 The Three-Stage Cyclonic Filtration Architecture Explained
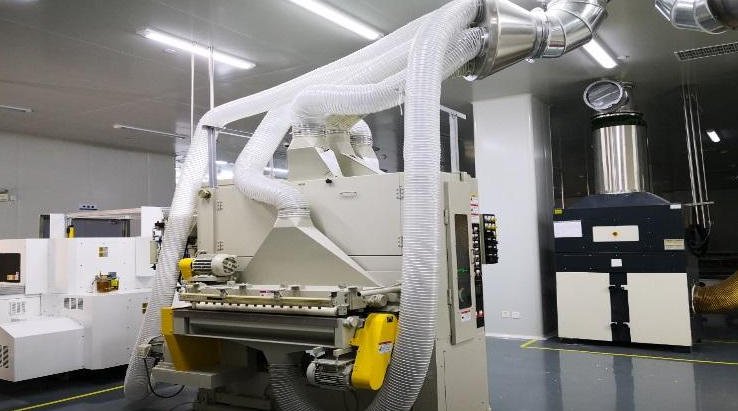
If fine quartz dust hits your final H13 filter directly, the cartridge will choke in fifteen minutes. That is why every heavy-duty Havenseek H13 HEPA vacuum cleaner relies on a three-stage cyclonic filtration architecture. First, a tangential steel inlet spins the airstream into an integrated non-clogging cyclonic pre-separator, forcing 92% of heavy abrasive grit straight down into the collection bag via centrifugal force.
5.2 Why Conical PTFE-Coated Pre-Filters Outperform Flat Cartridge Designs by 300%
Second-stage filtration handles the remaining 8% of fine suspended powder before it ever touches the HEPA stage. Instead of cheap polyester bags, we install a high-surface-area conical PTFE coated pre-filter rated at M-Class (99.9% down to 1 micron). Because expanded Polytetrafluoroethylene has an ultra-slick microscopic membrane, sharp silica crystals cannot hook into the fibers, extending filter life by 300%.
5.3 Reverse Pulse Jet Filter Cleaning: Purging Silica Cake Without Stopping the Grinder
In Stage Three, air passes through isolated H13 HEPA cartridges mounted above the main chamber. To keep suction constant without opening the tank, our reverse pulse jet filter cleaning system fires a sudden atmospheric shockwave backward through the conical pre-filter. Operators simply lift a dual-chamber lever for three seconds, blasting caked concrete dust down into the drop-down bag while the turbine keeps running.
6. Powerplant Architecture: Single-Phase Bypass Turbines vs. Three-Phase Regenerative Blowers
Choosing the wrong motor setup is the fastest way to burn out an H13 HEPA vacuum cleaner on a demanding jobsite. Your powerplant selection depends entirely on whether your crew moves between residential renovation sites or operates stationary 24/7 industrial production lines.
6.1 Multi-Motor Ametek Lamb Bypass Systems for Mobile Jobsite Agility
For portable surface prep where only 110V or 230V single-phase power exists, we equip our units with two or three independent multi-motor bypass Ametek Lamb turbines. Bypass cooling means dirty vacuum air never touches the carbon brushes; a separate cooling fan draws clean room air over the copper windings.
- Independent Switching: Run 1, 2, or 3 motors to match amp limits on standard 15A/20A breakers.
- Service Life: 1,200 to 1,500 operating hours before simple carbon brush replacement.
6.2 Continuous-Duty Three-Phase Side-Channel Blowers for 24/7 Factory Production
For large planetary floor grinders or stone CNC machines running triple shifts, carbon brushes wear out too fast. We mount a die-cast aluminum three-phase brushless regenerative blower (4.0 kW to 7.5 kW, 380V–480V) directly to the lower chassis for rock-solid center of gravity.
- Zero Friction Wear: Impeller rotates without mechanical contact, delivering 30,000+ maintenance-free hours.
- High Vacuum Torque: Sustains up to 125 inches of water lift without overheating under heavy silica loads.
7. Safe Disposal Engineering: Eliminating Secondary Exposure During Bag Changes
7.1 How the Continuous Longopac Bagging System Traps Toxic Dust Until Disposal
What good is capturing 99.95% of toxic dust if your worker dumps an open steel bin into a dumpster and inhales a massive cloud of silica? Under modern workplace air quality standards, open-drum dumping is a guaranteed way to fail personal breathing-zone monitoring.
Every Havenseek compliant dust extractor integrates a gravity-fed hopper equipped with a continuous Longopac bagging system. This 22-meter pleated polyethylene sleeve sits around the discharge cone. When a section fills with 20 kg of concrete powder, the operator pulls down fresh tubing, seals the top with two heavy-duty zip ties, and cuts between them—achieving 100% contact-free, sealed disposal.
8. How Much CFM Do OSHA Silica Dust Rules Require for Concrete Grinders?
8.1 Mastering the 25 CFM Per Inch of Grinding Wheel Diameter Rule
During equipment consultations, the number one question contractors ask is: How much CFM do OSHA silica dust rules require for concrete grinders? If you follow OSHA Table 1 to avoid mandatory air monitoring, federal law mandates a minimum airflow of 25 CFM per inch of grinding wheel diameter.
The math is straightforward but unforgiving. A 5-inch hand-held angle grinder requires at least 125 CFM, while a 7-inch cup wheel demands 175 CFM. Step up to a 20-inch walk-behind planetary grinder, and your H13 HEPA vacuum cleaner must deliver a minimum of 500 CFM of sustained airflow to prevent dust from escaping under the brush skirt.
8.2 Static Pressure (Water Lift) vs. Airflow (CFM): Why High CFM Alone Fails on Long Hoses
Here is what 90% of spec sheets hide from you: balancing static pressure water lift vs airflow CFM. CFM (Cubic Feet per Minute) measures air volume with no hose attached, while Water Lift (measured in inches of H2O or kPa) measures raw suction force against friction. If you attach a 25-foot, 2-inch hose to a fan-style collector with high CFM but weak water lift (under 60 inches), hose friction cuts real airflow at the grinder shroud by more than 55%.
9. Comprehensive Tool-to-Vacuum Matching Guide (With Comparison Matrix Table)
9.1 Hand-Held Angle Grinders, Tuckpointers, and Walk-Behind Saws (150–250 CFM Tier)
For mortar tuckpointing, joint chasing, and 5-to-9-inch hand grinding, portability and high air velocity matter most. A dual-motor 2.4 kW single-phase H13 HEPA vacuum cleaner producing 235 CFM and 100 inches of water lift easily handles one 7-inch grinder or two 5-inch grinders via a Y-splitter without tripping standard 20-amp jobsite breakers.
9.2 Heavy-Duty Planetary Floor Grinders and Scarifiers (350–650+ CFM Tier)
High-production concrete planetary floor grinder dust collection generates up to 80 kg of micro-fine powder per hour. Pairing a 25-inch or 32-inch grinder with a small single-phase vac will choke the hose in minutes. You need a three-motor 3.6 kW unit (380 CFM) or a 5.5 kW–7.5 kW three-phase turbine unit pushing 450 to 650 CFM through a 3-inch main trunk hose.
| Application & Grinding Tool | Min OSHA CFM | Recommended Vacuum Tier | Min Water Lift | Pre-Filter & H13 Area |
|---|---|---|---|---|
| 5″–7″ Hand Grinder / Tuckpointer | 125–175 CFM | 2.4 kW Dual-Motor 1-Phase | 98 inH2O (24.5 kPa) | 3.0 m² PTFE + 2.4 m² H13 |
| 10″–14″ Early-Entry Concrete Saw | 250–350 CFM | 3.6 kW Triple-Motor 1-Phase | 102 inH2O (25.4 kPa) | 4.5 m² PTFE + 3.6 m² H13 |
| 20″–24″ Planetary Floor Grinder | 400–520 CFM | 5.5 kW 3-Phase Turbine | 115 inH2O (28.6 kPa) | 6.2 m² PTFE + 5.0 m² H13 |
| 30″–32″ Ride-On Grinder / Scarifier | 600–750 CFM | 7.5 kW 3-Phase + Front Cyclone | 128 inH2O (32.0 kPa) | 8.5 m² PTFE + 7.2 m² H13 |
9.3 Pros and Cons of Auto-Pulse vs. Manual Jet-Pulse Compliant Dust Extractors
- Pro: Zero fragile PCB circuit boards or solenoid valves to fail in humid, dusty environments.
- Pro: Costs 25% less upfront and requires zero external air compressor hookups.
- Con: Relies on the operator remembering to pull the purge handle every 20 to 30 minutes.
- Pro: Alternately blasts multi-chamber filters every 45 seconds for 100% hands-free grinding.
- Pro: Essential for automated CNC stone routing and robotic floor preparation.
- Con: Higher initial purchase weight and requires periodic drainage of internal compressor moisture.
10. Jobsite Setup & Accessories: Hose Diameter, Grounding, and Shroud Integrity
10.1 Preventing Electrostatic Shocks with Anti-Static Conductive Vacuum Hoses
When dry quartz particles travel through a plastic hose at 85 miles per hour, triboelectric friction generates up to 25,000 volts of static electricity. Without an anti-static conductive vacuum hose grounded directly to the steel chassis of your H13 HEPA vacuum cleaner, operators suffer painful electric shocks that cause them to drop spinning angle grinders.
10.2 Optimizing Brush Skirts on Heavy-Duty Concrete Grinding Dust Shrouds
Even a 600 CFM extractor will fail inspection if your tool shroud leaks. Always pair your machine with a heavy-duty concrete grinding dust shroud featuring replaceable double-row nylon brush skirts or flexible polyurethane lips. If a gap wider than 3mm opens between the shroud and uneven concrete, high-velocity dust shoots sideways out of reach of the vacuum port.
10.2.1 Reading the Differential Pressure Gauge Manometer to Time Your Filter Purges
Never guess when your pre-filter needs cleaning. Every Havenseek unit features a front-mounted liquid-filled differential pressure gauge manometer wired across the clean and dirty sides of the filter bulkhead. When internal resistance climbs into the amber zone (above 18 kPa), operators know immediately to trigger the reverse pulse lever before airflow drops below OSHA thresholds.
11. Real-World B2B Case Studies: Before-and-After Air Quality & ROI Audits
11.1 Case Study A: Midwest Commercial Concrete Contractor Cuts Silica Exposure by 94%
In early 2025, an Ohio commercial flooring contractor running six 24-inch grinders failed an independent industrial hygiene audit with breathing-zone readings of 142 μg/m³—nearly triple the legal limit. Their existing single-stage vacuums suffered from warped plastic latches and clogged paper filters every forty minutes.
We replaced their fleet with six Havenseek 5.5 kW three-phase extractors paired with front-mounted cyclone pre-separators. Follow-up gravimetric sampling confirmed exposure dropped to 8.5 μg/m³ (well below the 25 μg/m³ Action Level), while annual filter replacement and labor downtime costs dropped by $18,400 across the six crews.
| Audit Metric (Ohio Fleet of 6 Grinders) | Before (Generic Vacuums) | After (Havenseek H13 + Cyclone) | Net Operational Impact |
|---|---|---|---|
| 8-Hour TWA Silica Exposure | 142.0 μg/m³ (Non-Compliant) | 8.5 μg/m³ (Fully Compliant) | -94.0% Dust Reduction |
| Filter Cleaning Downtime / Shift | 65 Minutes / Crew | 6 Minutes (Jet-Pulse) | +5.9 Productive Hours / Day |
| Annual Filter Consumable Spend | $14,200 / Year | $3,150 / Year | $11,050 Direct Parts Savings |
11.2 Case Study B: Australian Quartz Countertop Fabricator Passes Surprise WorkSafe Audit
Engineered stone and sintered porcelain slabs contain up to 90% crystalline silica. A Melbourne fabrication shop facing strict WorkSafe Victoria enforcement implemented our strict airborne silica dust monitoring protocol alongside twelve mobile H13 extractors for their dry-polishing booths. Zero detectable bypass leakage allowed them to pass three consecutive unannounced government air audits with zero citations.
12. 5 Costly Mistakes B2B Buyers Make When Sourcing Industrial Dry Dust Extractors
12.1 Mistake #1: Trusting “Free-Air CFM” Instead of “Loaded CFM at the Shroud”
Many trading companies test airflow with the filter removed and no hose connected. Always demand the “loaded CFM curve” measured through a 25-foot hose with a partially loaded PTFE filter. A genuine H13 HEPA vacuum cleaner maintains at least 78% of its rated airflow even after two hours of continuous concrete grinding.
12.2 Mistake #2: Ignoring Filter Replacement Intervals and Total Cost of Ownership
Saving $300 on a cheap machine makes zero sense if it burns through $1,800 worth of proprietary paper cartridges every six months. Standardizing your fleet around washable or pulse-cleanable conical PTFE pre-filters cuts your three-year Total Cost of Ownership (TCO) in half.
12.3 How Often Should You Replace Filters in a Compliant Dust Extractor?
Fleet managers frequently ask: How often should you replace filters in a compliant dust extractor? Under daily concrete grinding conditions (6 hours per day), a conical PTFE pre-filter lasts 9 to 12 months, while the secondary H13 HEPA cartridges should be replaced every 6 to 9 months—or immediately if the manometer stays above 20 kPa after pulse purging.
12.4 Does an H13 HEPA Vacuum Cleaner Eliminate the Need for Respiratory Protection Under OSHA Table 1?
To stay completely transparent, buyers often ask: Does an H13 HEPA vacuum cleaner eliminate the need for respiratory protection under OSHA Table 1? For outdoor grinding or indoor walk-behind floor grinding, a properly rated extractor requires zero respiratory protection under Table 1. However, if operators use hand-held angle grinders indoors or in enclosed spaces for more than 4 hours per shift, OSHA still requires wearing an APF 10 half-mask respirator alongside your vacuum.
13. Frequently Asked Questions (Schema-Ready B2B Buyer FAQ)
Q1: Can I wash an H13 HEPA filter cartridge with water or compressed air to save money?
Never wash or blow out an H13 HEPA cartridge with high-pressure shop air. Water destroys the electrostatic charge and tears microscopic borosilicate glass fibers, while 100 PSI air guns punch invisible pinholes through the pleats. You may gently rinse the primary PTFE pre-filter if rated washable, but H13 cartridges must always be replaced dry.
Q2: What is the minimum order quantity (MOQ) for private-label compliant dust extractors?
At Havenseek Industrial Vacuum Cleaner, we support regional distributors and equipment brands with low-MOQ private-label programs starting at just 5 to 10 units per model. We offer custom powder-coated chassis colors, laser-engraved serial plates, and custom-branded cartons for global B2B wholesale buyers.
Q3: How do I verify if a supplier’s EN 1822 H13 certificate is authentic?
Check three details on the report: first, ensure the testing standard specifically states EN 1822-1:2019 or ISO 29463; second, verify that the aerosol test substance is DEHS or PAO measured at MPPS (0.15–0.3 microns); third, confirm each physical cartridge carries a unique tracking barcode matching the test sheet.
Q4: Why does my vacuum lose suction after 20 minutes of grinding concrete?
Rapid suction loss happens when fine silica dust embeds inside non-coated cellulose or polyester filters—a phenomenon called “filter blinding.” Switching to an H13 HEPA vacuum cleaner with a tangential cyclonic inlet and a hydrophobic PTFE membrane pre-filter stops dust from sticking to the pleats.
Q5: What voltage options are available for North American vs. European/Australian markets?
We manufacture full regional electrical configurations: 110V–120V (60Hz) and 220V–240V single-phase, plus 208V/230V/460V/480V (60Hz) for North America, and 230V (50Hz) single-phase or 380V–415V (50Hz) three-phase for Europe, the UK, Australia, and South America.
Q6: How does pre-separator cyclone efficiency impact H13 HEPA filter lifespan?
Adding a dedicated front-mounted cyclone separator removes 95% to 98% of pulverized concrete before the air stream enters the vacuum drum. In our field trials, pairing a pre-separator with a 3-motor extractor extends H13 cartridge lifespan from 6 months to over 18 months.
Q7: Are Havenseek dust extractors compliant with both OSHA 1926.1153 and EU Machinery Directives?
Yes. Every industrial model is engineered to exceed OSHA silica dust rules (29 CFR 1926.1153 / 1910.1053) for airflow and 99.95% filtration efficiency, while holding CE certification and EN 60335-2-69 H-Class / EN 1822 H13 compliance for European and global workplace air quality standards.
14. Conclusion: Future-Proof Your Fleet with Factory-Engineered Silica Compliance
Cutting corners on dust control is a gamble no serious contractor or equipment distributor can afford in 2026. When government inspectors step onto your jobsite, having a properly engineered H13 HEPA vacuum cleaner with verified DOP leak testing, EPDM compression seals, and non-clogging PTFE cyclonic filtration protects your workers, your reputation, and your bottom line.
Whether you are upgrading a concrete polishing fleet or sourcing private-label extractors for regional wholesale distribution, our engineering team at Havenseek Industrial Vacuum Cleaner will match your exact tool CFM, voltage, and compliance requirements directly from our factory floor.
- Occupational Safety and Health Administration (OSHA) – Crystalline Silica Rulemaking & Standard 29 CFR 1926.1153
- National Institute for Occupational Safety and Health (CDC/NIOSH) – Engineering Controls for Respirable Crystalline Silica
- Health and Safety Executive (HSE) – Construction Dust Control and On-Tool Extraction Standards